


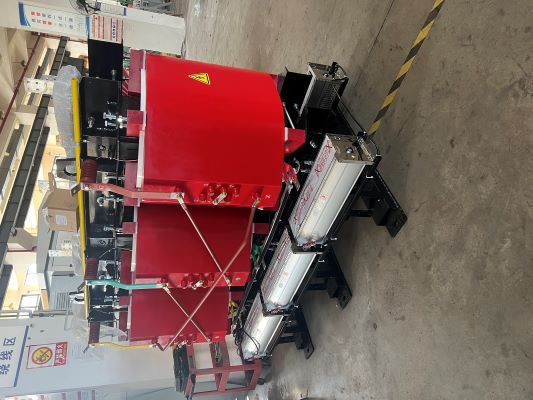
Transformer production process
The general operating steps of transformers are as follows:
1、Core processing, the core material is usually cold-rolled grain oriented electrical steel strip, and the appropriate grade of silicon steel sheet is selected according to the performance and application of the transformer, such as ordinary silicon steel sheet, high permeability silicon steel sheet, laser scored silicon steel sheet, etc. After selecting the iron core material, the iron core should be cut and stacked. The rolled electrical steel strip is subjected to "longitudinal cutting" and "transverse cutting" through professional cutting lines, and automatically stacked into iron core columns and iron yokes. The staggered stacking or step-by-step stacking method can be used, and step-by-step stacking can reduce the excitation current and no-load loss. Punching positioning holes on the iron core sheet can improve the stacking efficiency and quality of the iron core, but attention should be paid to the impact of punching on the performance of the silicon steel sheet.
2、Iron core assembly: After the iron core is processed, the stacked iron core columns and iron yokes are assembled together. For large capacity transformers, oil passages should be added to the iron core to control temperature rise. During assembly, it is necessary to ensure that the verticality of the iron core and the flatness of the laminations meet the requirements.
3、Winding is an important step, and the appropriate wires should be selected based on the voltage, capacity, and purpose of the transformer, such as rectangular oxygen free copper wires, circular wires, transposed wires, etc. The wires should have an insulation layer on the outside. Next, choose the winding method. Common winding types include layered, continuous, tangled, spiral, etc. Choose the appropriate winding method based on design requirements and the performance characteristics of the transformer. The winding method adopts semi-automatic or fully automatic winding machines to ensure that the number of turns, diameter, foot position, direction, etc. of the winding meet the design requirements. During the winding process, attention should be paid to the flatness of the wire package, tape width, sleeve length, etc. After the final winding is completed, the winding should be shaped to meet the size and shape requirements of the design, such as ensuring flatness between layers for layered windings and accurate transposition for continuous windings.
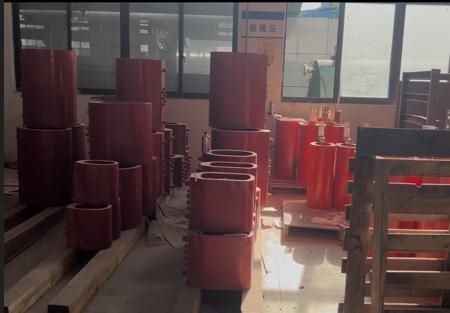
4、Choose insulation materials, commonly used insulation materials include insulation paper, insulation cardboard, electrical film, epoxy resin, etc. Choose the appropriate insulation material according to the insulation level and usage environment of the transformer. After selection, the insulation production workshop processes the insulation materials into various shapes and sizes of insulation parts, such as insulation cylinders, winding pads, partitions, cardboard cylinders, etc. These insulation parts are used to isolate windings from iron cores and windings from each other, ensuring the insulation performance of transformers. Finally, connect the winding assembly to the leads, mount the wound winding onto the iron core column, and insert the iron yoke laminations to ensure a tight fit and accurate position between the winding and the iron core.Connect the leads of the winding. Copper busbars or copper tubes are used instead of cables for high current and low voltage leads. The high voltage tap leads are led to the tap changer through cables, and the middle outgoing line of the high voltage head end is led to the high voltage bushing through insulated tubes. The leads and busbars should be firmly connected and have good electrical performance.
5、After the assembly of the body kit and leads, the entire iron core and winding are dried using gas-phase drying method to remove moisture from the insulation material and improve the insulation performance and stability of the transformer.
6、Fuel tank manufacturing generally uses Q235 steel, and non-magnetic steel is often used for the outlet sleeve position of the fuel tank cover to reduce eddy currents. Cut according to the design drawings of the fuel tank, and then machine the cut plates, such as cutting, bending, drilling, etc., to produce various components of the fuel tank. Weld and assemble the processed fuel tank components to ensure the sealing and strength of the fuel tank. After welding, perform weld seam inspection. Finally, the fuel tank should be painted as a whole, and shot blasting or sandblasting should be carried out before spraying the primer to improve the adhesion of the paint.
7、After completing the steps above 7, proceed with the final assembly of the transformer's various components, such as the body, oil tank, bushing, oil pillow, oil pump, fan, end control box, etc., to ensure that they are installed correctly and connected reliably.
8、The last and most important step is the acceptance stage of the entire process, which is testing: the transformer needs to undergo a series of strict tests, including routine tests, type tests, and special tests such as insulation resistance tests, dielectric loss tests, withstand voltage tests, partial discharge tests, no-load tests, short-circuit tests, etc., to verify whether the performance and quality of the transformer meet the standard requirements
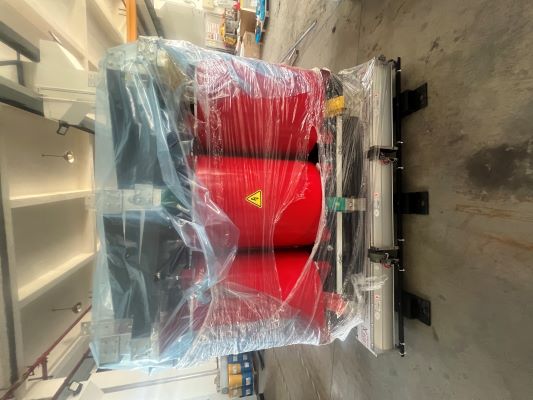
The above are all the steps involved in completing a transformer, but the production process may vary slightly depending on the transformer. For example, when insulating Dry-Type Transformers, it is necessary to mix epoxy resin with curing agent and pour it onto the coil or iron core to form a strong insulation layer.